For B2B buyers, a golf stand bag failure in the field almost always begins in the material spec — a 600D nylon shell with a 210D inner liner can differ by roughly 15-20% in abrasion resistance and cost, so knowing how to test denier, tear strength, and waterproofness before moulding your order is what protects your landed quality. This guide gives brand teams and distributors a repeatable testing framework for golf stand bag materials, using the inspection standards and tolerances our SGS-verified Quanzhou facility (founded 2014, 20 years of industry experience, 4,950 sqm, 7 lines, 149 machines, 137 staff, 200,000-unit monthly line capacity) applies on every fabric lot that moves through bulk production. For the wider golf bag category — cart bags, staff bags and more — our affiliated golf bag factory is the one-stop reference.
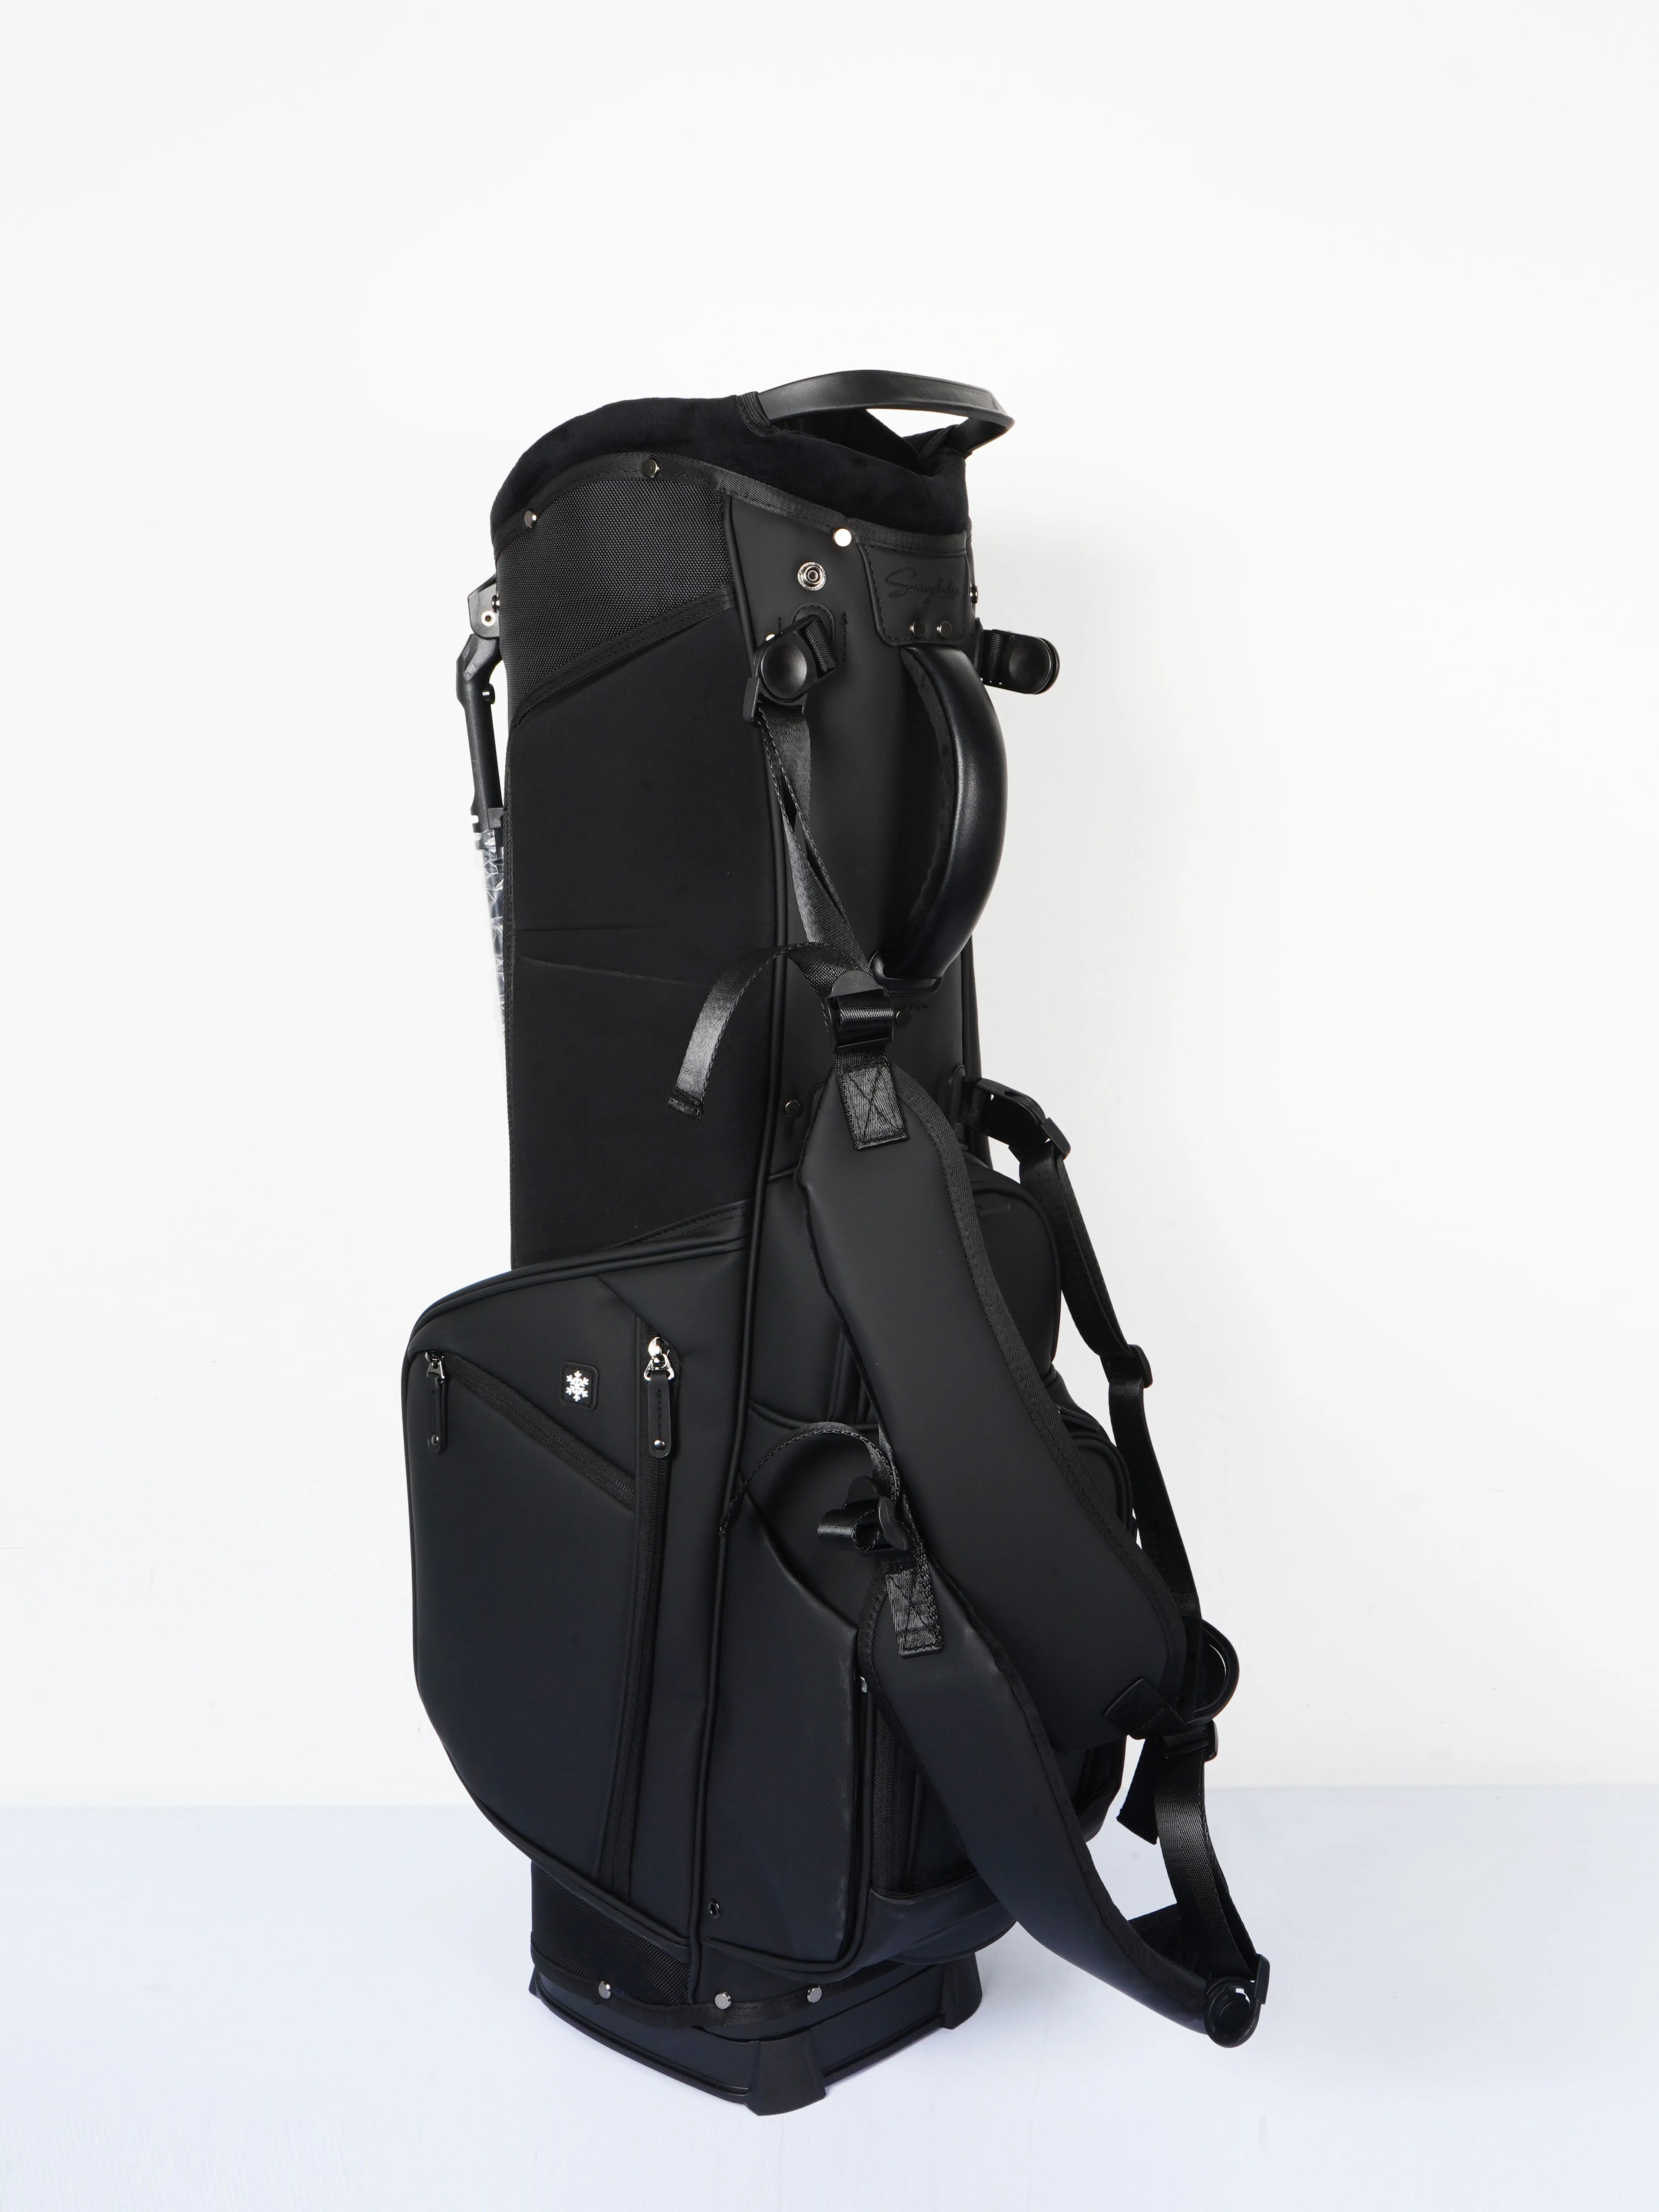
Key Takeaways
- Materials test in layers: shell, liner, reinforcement, hardware, and stand frame each have separate acceptance criteria.
- Denier and weave dictate 60-70% of shell performance; moving 210D to 600D can raise abrasion survival by several multiples at a modest weight penalty.
- Standardised tests to agree on: Martindale/Taber abrasion, tongue tear, tensile grab, hydrostatic head, and seam strength.
- Water resistance is on a scale — splash (hydrostatic head) is not the same as fully sealed waterproof construction.
- Lock a lot-release test on the first 3-5 rolls of every material batch before cutting begins.
Why Material Quality Fails Before the Bag Does
Most buyers judge a stand bag by how it feels in a five-minute inspection, but material failure is a slow process that shows up at week forty, not day one. The shell abrades at the contact points where the bag rubs against the cart and the ground. The liner tears around the club tips where graphite and steel shafts hammer it on every walk. The waterproof membrane delaminates from cold, repeated flexing at the divider rails. None of these failures are visible at the sample stage unless the buyer is testing the right parameters on the right panels. That is why a material testing protocol is worth building before, not after, a bulk order.
Working with an affiliated plant that already runs AQL lot-release checks shortens this learning curve. Our Quanzhou facility tests incoming rolls against a frozen master before cutting, so a material defect is caught at the goods-inward stage rather than after four hundred bags are half-sewn. Every season we see the same three causes of rework: a sub-standard lining roll that was not tested against the approved spec, a PU coating batch that delaminated because the adhesion peel test was skipped, and a zipper tape lot that gummed up because only the teeth, not the tape and slider, were checked. Build these three checks into your material protocol and you eliminate the majority of field warranty claims.
Denier, Weave, and What the Numbers Really Mean
Denier is simply the weight in grams of 9,000 metres of a fibre; higher numbers mean thicker, heavier, and usually tougher yarn. A 210D liner is light and flexible, a 420D shell balances weight and strength, and a 600D or 840D shell is the workhorse of hard-wearing bags. But denier alone is a poor predictor of abrasion because a tightly woven ripstop construction resists tearing far beyond a plain weave of the same denier. A 600D ripstop with a 1-in-4 grid of nylon rip-stop yarn will stop a tear from running across a panel, which is why we specify ripstop for stress zones like the base and the stand hinge surround.
Weight, quoted in grams per square metre (gsm), matters for the buyer's target bag weight. A typical stand bag shell is 180-260 gsm for 600D nylon, while a premium PU-coated nylon can run 300-400 gsm depending on the coating add-on. When you compare two quotations, never compare only per-unit price; compare denier, weave, gsm, and finish. Two "600D" bags can differ by 30% in real strength if one uses a loose mine-weave with a thin coating and the other a tight ripstop with a polyurethane backcoating. Our affiliated plant holds every shell type to a written spec and records the gsm on the lot-release report.
Reading a Material Spec Sheet Like a Factory
A professional fabric spec sheet lists seven numbers the factory will hold you to: composition, denier, weave or construction, gsm, tensile strength, tear strength, and any coating or finish. If a supplier sends you a sheet with only "600D nylon, PU coated" and no test numbers, treat it as a starting point, not a guarantee. Ask specifically for the test method next to each value, because ASTM tongue-tear results are not directly comparable to ISO or GB/T results. The method and the fabric direction (warp vs weft) must be written on the sheet or the number is meaningless in negotiation.
We keep a signed material spec for every shell in our catalogue and share it with approved buyers prior to sampling. When you request a material trial, ask the factory to confirm the spec sheet, produce a 30 cm by 40 cm swatch of the approved lot, and run the four core tests described below on that exact swatch. This is how you lock repeatability before the first production run, and it is exactly the discipline that keeps a reorder shipping at the same physical quality as the original.
Test 1 — Abrasion Resistance
Abrasion is the number-one field-failure mode for stand bags because the base and lower panels drag over concrete, cart rails, and sandy paths. The two common methods are the Taber abraser and the Martindale. The Taber machine rotates a specimen under two abrasive wheels and records cycles before the surface shows a defined amount of wear; the Martindale rubs fabric in an Lissajous pattern and is more common for coating and lining wear. For stand bags we typically target 20,000 to 50,000 cycles depending on the segment, always with the method named so the number is a real target rather than marketing.
Pay attention to what "failure" means in the test — some suppliers stop the machine at the first broken yarn while others run until the coating separates. Agree on the stop condition in writing. A 600D ripstop with a PU backcoating will usually survive more cycles than the same bag in a thin 210D lining, which is why we always test the base panel, not the gusset, and record whether the tear stopped at a rip-stop thread. This single test, run on the real production lot, catches most of the "my bags wore through in a season" complaints that end up as warranty claims.
Test 2 — Tear and Tensile Strength
Tear strength measures how a running tear propagates once a panel is cut or snagged, and the tongue-tear test (ASTM D2261) is the standard we rely on for stand bag shells. Tensile strength, sometimes measured by the grab method (ASTM D5034), tells you how much load the fabric holds before it breaks. For a golf stand bag, tear strength matters more than tensile because every bag gets snagged on branches, cart edges, and the occasional protruding pipe; a bag with high tensile but low tear strength will pop a long rip the first time it catches.
A practical target for a 600D nylon shell is a tongue-tear value in the range of 25-50 N in warp and weft, with the exact figure set by the panel and segment. The reinforcement we specify at the base, the divider-tube entry, and the stand hinge surround typically uses a heavier weave or a double layer, and we run a tear test on those seams too. When you review a lot release, confirm the tear direction and the test method, and ask for the number on the reinforced panels, not just the plain shell — that is where a weak design really becomes a warranty problem.
Test 3 — Water Resistance and Waterproofness
Water performance sits on a scale. A splash-resistant bag with a polyurethane backcoating keeps light rain off the contents for a while but is not sealed. A genuinely waterproof bag uses a TPU laminate or a welded construction with sealed seams and water-resistant zippers. The simplest objective measure is the hydrostatic head test, which records how many millimetres of water the fabric holds before water penetrates. A plain backcoated shell might measure 300-800 mm; a serious waterproof stand bag targets a hydrostatic head of 5,000-10,000 mm or more on the sealed panels.
Do not confuse a coated shell with a waterproof system. Water will find the seams, the zipper teeth, and the pocket joins long before it defeats the fabric itself. Test water resistance on the finished panel: pour, drip, or hose the assembled seam area and check the sewn line, not just the flat centre of the fabric. Our affiliated plant seals the critical seams on waterproof programs and verifies them with a short shower-booth test on the first article of each run, so a buyer can trust the water claim in the sales description as well as in the lab report.
Test 4 — Seam Strength and Stress-Point Reinforcement
A bag fails at the seams before it fails through the fabric. Seam strength is tested by clamping two sewn panels and pulling until the stitch row or the fabric gives way. The acceptance target depends on the seam type and panel; for a main body seam on a stand bag we generally look for no stitch breakage at the stated load and no fabric slippage beyond a defined amount. The worst seam failures come from an under-specified stitch count per inch, a weak thread, or a seam that runs perpendicular to the direction of load at a stress point like the hip pad or the stand hinge anchor.
Stress-point reinforcement is where the design earns its keep. The hip pad anchors, the dual-strap attachment points, the bottom wear plate, and the divider-tube entry all take concentrated load, and each should be reinforced with a bar tack, a heavier internal webbing piece, or an extra stitch row. When you inspect a sample, pull each anchor by hand and watch where the fabric puckers first; that pucker predicts the failure location. Spec the reinforcement in the tech pack and put a seam-strength target in the QC plan, so the sample you approve is the production the factory has to match.
Material Test Parameter Table
Below is the lot-release parameter sheet we use at our affiliated plant for a typical mid-tier carry stand bag. Use it as your negotiation baseline and lock the final numbers with the factory before bulk.
| Test | Common Method | Mid-Tier Starting Target | Buyer Note |
|---|---|---|---|
| Shell composition / denier | Yarn count, fabric construction | 600D nylon ripstop, 180-260 gsm | Confirm weave and warp/weft on sheet. |
| Abrasion | Taber / Martindale | 20,000-50,000 cycles | State the stop condition (first yarn break / coating loss). |
| Tongue tear | ASTM D2261 | 25-50 N warp and weft | Test reinforced panels too. |
| Tensile (grab) | ASTM D5034 | Define by segment | Set method and direction. |
| Seam strength | Clamped seam pull | No split at stated load | Test hip pad, strap anchors, hinge surround. |
| Water resistance | Hydrostatic head mm H2O | Backcoated 300-800 mm | Waterproof programs target 5,000-10,000 mm + sealed seams. |
| Colour fastness | AATCC / ISO grey scale | Specify wash & light level | Set delta-E on approved chip. |
| PU coating adhesion | Peel / rub test | No delamination at stated cycles | Critical on coated and laminated shells. |
PU Synthetic Leather and Coated Materials
On premium and tour-level stand bags, PU synthetic leather panels add a refined feel and a more expensive shelf appearance, but they bring a different failure mode: the PU coating can crack, flake, or delaminate from the base fabric with repeated flexing and heat. A good PU-coated nylon should survive the same dry-flex count as the shell and show no surface cracking at the hinge zones. Test the coating on the actual fold line where the bag bends during stand deployment, because that is where a weak coating reveals itself.
When a buyer specifies PU panels, ask for three numbers: the base fabric composition, the PU coating thickness and add-on, and the adhesion value from a peel or rub test. Also confirm the finish — smooth, embossed, or a soft-touch matte all behave differently under abrasion. The premium look is only valuable if the coating survives a season of real use, which is exactly why our lot-release protocol includes a dry-flex and a rub check on the coated panels before they go to the cutting table.
Zippers, Hardware, and Stand-Frame Materials
Materials testing does not stop at the fabric. The zipper tape, teeth, slider, and pull each need a cycle test to check for jamming, rough pull force, and tape fraying; we target 3,000 to 10,000 zipper cycles depending on the position, tracking pull force and jam rate. Hardware — clips, buckles, strap slides, and the stand hinge — should be checked for plating and corrosion resistance, with a salt-spray test on the metal parts if they will see coastal or sweaty use. The stand frame itself is typically steel or aluminium tubing; a buyer should confirm the tube grade, wall thickness, and the deployment spring or cam mechanism, and run a deployment cycle test to ensure consistent spread and no cracking at the hinge.
The interlock between fabric and hardware is where many recalls hide. A strap webbing that is strong on paper but sewn with a weak thread will part at the stitch row, so the strap-anchor load test must include the stitching, not just the webbing. Similarly, a zipper slider that feels smooth on a cut sample can jam on the finished bag if the pocket panel distorts during sewing. This is why we test finished assemblies, not isolated components, on the first article — a composite check you should insist on before approving any production sample.
Test Plan & Acceptance Criteria
For professional programs, add test methods and pass/fail criteria to the tech pack so there is no ambiguity at inspection.
- Lot-release on first 3-5 rolls: gsm, tear, tensile, abrasion, coating adhesion.
- Seam-strength pull at hip pad, strap anchors, and stand hinge surround.
- Zipper cycle test with pull-force and jam-rate targets.
- Hardware salt-spray check if the target market is coastal or humid.
- Water-resistance verification on waterproof programs: hydrostatic head plus seam seal shower test.
- Stand deployment cycle test with no-cracking, no-severe-wobble criteria.
- Record a sealed master and first-article report on run #1.
What to Send the Factory for a Material Trial
The fastest way to a clean material trial is to send a one-page material brief alongside your RFQ. State your target segment and resale price, the bag type (lightweight carry, 14-way, waterproof, hybrid), the target weight and tolerance, the material direction (nylon, polyester, PU, TPU waterproof), the packout and branding plans, your required test methods, and your inspection level. The more measurable targets you declare, the faster the factory can quote and the fewer ambiguity-driven rework loops you will pay for.
At our Quanzhou facility, material sampling typically runs 10-20 days and bulk production 45-60 days; an early, complete material brief lets us lock the shell, lining, and hardware in one sampling round instead of three. We encourage approved buyers to request the sample's lot-release report with their evaluation sample, so you are not approving a beautiful one-off but a reproducible lot. If you are assessing a factory's process maturity, this report is the single most revealing document it can show you.
Procurement Worksheet
Use this worksheet to collect material inputs before you send an RFQ.
| Requirement | Your Target | Notes / Questions |
|---|---|---|
| Shell composition / denier | Nylon / polyester / PU / TPU; ripstop or plain. | |
| Shell gsm & finish | Backcoated, PU peel-coat, laminated, soft-touch? | |
| Liner material | 210D-420D nylon; consider club-tip abrasion. | |
| Abrasion / tear / tensile targets | Nominate method and stop condition. | |
| Water level | Splash-resistant vs fully waterproof; hydrostatic head target. | |
| Hardware & zipper standard | Brand, cycle target, plating/salt-spray. | |
| QC & testing | AQL level plus material lot-release. | |
| MOQ & lead time | First-order quantity, reorder plan, timeline. |
Sampling & QC Checklist
Use this list to align expectations before sampling and before bulk production.
- Target market, price positioning, and resale segment.
- Bag architecture, weight, and material direction.
- Signed material spec with named test methods and values.
- 30x40 cm swatch of the approved lot plus lot-release report.
- Waterproof scope, seam-sealing method, and hydrostatic head target.
- Hardware, zipper, and stand-frame material standards.
- AQL checkpoints and material lot-release on every bulk lot.
Recommended Internal Links
- Products (Stand Bag Architectures)
- OEM/ODM Service
- Factory & QC
- Golf Stand Bag Buying Guide
- PU Synthetic Leather Guide
- How to Verify a Factory
FAQ
What is the most important material test for a golf stand bag?
Abrasion resistance at the base and lower panels is the most common field failure, followed closely by tear strength at snag points. Run both with the method and stop condition named, and test the reinforced panels, not just the plain shell.
How do I know if a material is truly waterproof and not just coated?
Ask for the hydrostatic head value in millimetres (waterproof programs target 5,000-10,000 mm or more) and confirm the seams are sealed. A coated shell without sealed seams leaks along the stitch lines and zippers regardless of the fabric value.
Can two different mills call the same fabric "600D nylon" yet deliver different quality?
Yes, and by a wide margin. Weave (ripstop vs plain), gsm, coating add-on, and yarn quality all vary. Ask for the signed material spec with test method and values, plus a 30x40 cm swatch of the actual production lot, before you compare prices.
Which abrasion standard should I request — Taber or Martindale?
Either is acceptable as long as it is written on the spec and the stop condition is defined. Taber is common for coated shells; Martindale is often used for lining and coating wear. The number only means something when the method accompanies it.
Do I need to test the material on every reorder lot?
Yes, at least a reduced lot release on the first several rolls of each shell, lining, and hardware batch. Dye lots and coating batches vary, so a reorder without a lot check can drift in strength and colour, as covered in our reorder-consistency guide.
How do you support OEM/ODM material selection for golf stand bags?
We support OEM (branding on proven architectures) and ODM (co-developing structure, materials, pockets, and hardware). Send your target market, quantity, and material direction, and our affiliated Quanzhou plant will confirm the spec and run a lot-release test before bulk.
Request a B2B quote for golf stand bags
Send your target market, expected MOQ, and reference photos. We respond within 24 hours with a sampling plan.