For B2B buyers of custom golf stand bags, the working MOQ from our Quanzhou operation is 200 pieces per model per colorway, with a 100-piece test order accepted for first-time brand validation, sampling at 10-20 days and bulk production at 45-60 days. This guide explains what actually drives that minimum, how to structure your first order so you do not overstock, and the QC checkpoints our SGS-verified affiliated plant (4,950 sqm, 7 lines, 149 machines, 137 staff) uses to keep every unit within tolerance. For the wider golf bag category — cart bags, staff bags and more — our affiliated golf bag factory is the one-stop reference.
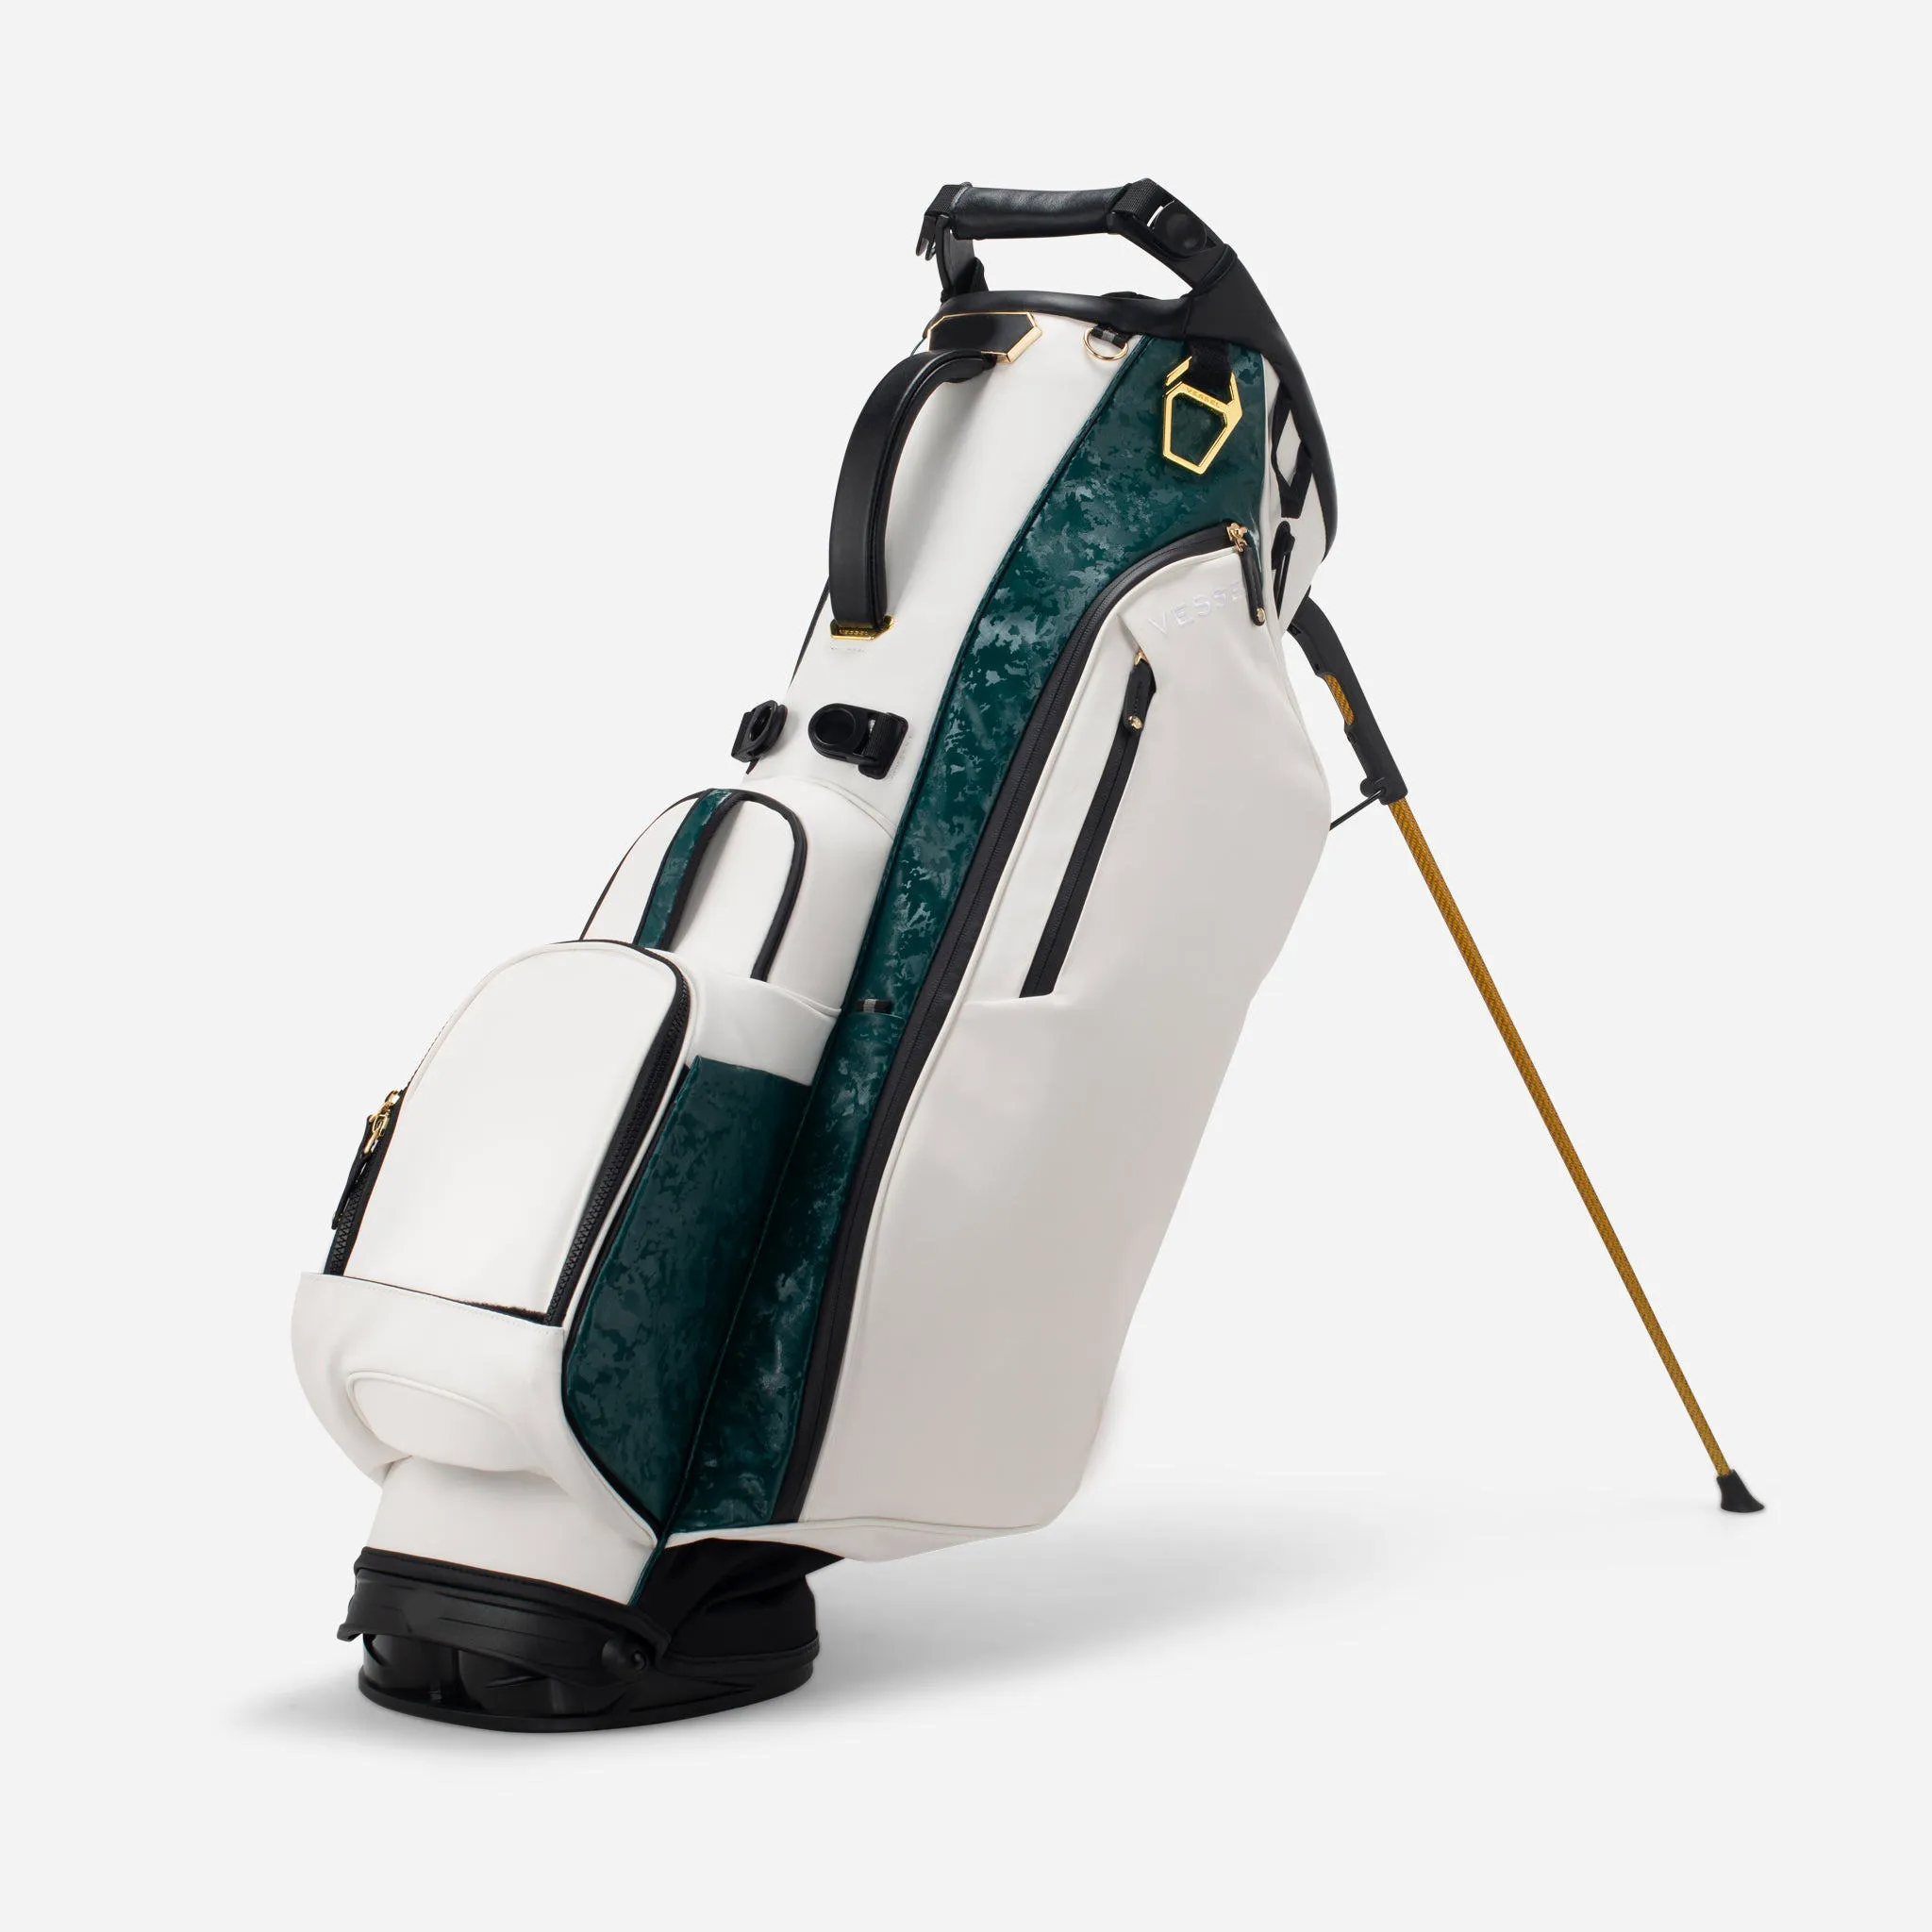
Key Takeaways
- Regular MOQ is 200 pieces; a 100-piece test order is available for first-timers.
- Sampling runs 10-20 days; bulk production runs 45-60 days at ~150,000 bags a month.
- Why 14-way dividers and waterproof TPU can push MOQ slightly higher.
- How to plan colorways and SKUs to stay above the minimum without bloating inventory.
- The QC records that make a reorder cheap and repeatable.
Why the MOQ Exists — and What It Buys You
A factory minimum is not an arbitrary gate; it reflects the fixed setup cost of a production run. When our affiliated plant switches to a new model, a new colorway, or a new set of hardware, it must rebuild the cutting marker, load the correct zipper and buckle stock, recalibrate the sewing machines, and run a first-article check. Those steps cost roughly the same whether you order 50 bags or 5,000, so the per-unit price collapses past a certain quantity while the setup cost has to be recovered.
At 200 pieces we can justify that setup and still hold a stable color from the dye lot and a consistent stitch standard. Below about 100 units, the fixed cost becomes a large fraction of every bag, the color batch risk rises because the dye lot is smaller, and the factory has little room to absorb rework. Understanding this is the first step to negotiating a sensible first order instead of being surprised at quote time.
It is worth stressing that MOQ and price per unit move together. In practice a 200-piece run gives a materially better unit price than a 100-piece pilot, and a 600-1,000 piece run unlocks another step down because the materials are bought in full rolls and the lines are set for a longer run. We publish our standard walls at the affiliated plant and quote each program on its own material and structural complexity.
Regular MOQ vs. Test Order — When to Use Each
Many first-time buyers assume they have to commit to a container. In our experience the smartest entry is a deliberately small test order of 100 pieces. That is enough to validate the physical bag, photograph it for your retail listing, test the fit of your logo on the real fabric, and gather early sell-through data — without tying up working capital on a colorway that may not move.
The regular 200-piece MOQ is the reliable planning number once you have validated the silhouette. It is the point where the economics of cutting, sewing, and hardware setup work cleanly and where we can hold a full AQL-driven inline inspection. Think of the sequence this way: test order proves the design, regular MOQ proves the repeatability, and a longer 600-1,000 piece run proves the cost curve. Each step feeds the next, and the QC records from the pilot are exactly what let you scale confidently.
If you are sourcing multiple retailers or a catalog, treat each colorway as a separate MOQ consideration. A grey and a navy panel are different dye lots, so a single model in three colors is effectively three minimums. Keeping the first season to one architecture and two to three colorways is the fastest way to stay stacked safely above the minimum.
How Structure and Material Shift the Minimum
Not every stand bag costs the same to set up. A basic 4-way carry bag on 600D polyester is our fastest, most economical build, and it sits firmly at the 200-piece standard. The moment you ask for a full-length 14-way divider system, the top assembly grows more complex: each divider tube must be sewn and aligned, and the lid pattern changes. Waterproof TPU panels add a lamination and heat-seal step that touches the whole shell. Both push the material order and setup cost up, and in a few cases we recommend a slightly higher minimum to protect color and seam integrity.
Hardware is another lever. A dual self-balancing strap, a reinforced hinge block, and premium YKK-class zippers all carry their own minimum buying quantities. When a buyer mixes high-cost hardware with a very small order, we flag it early so they can decide whether to expand quantity or simplify hardware. The honest conversation at quote time prevents a disappointing per-unit number later.
For a compact vinyl-coded summary, the table below shows how our MOQ behaves across the common stand bag configurations so you can plan your first season realistically.
| Configuration | Regular MOQ | Notes |
|---|---|---|
| Basic 4/5/6-way, 600D polyester or nylon | 200 pcs | Fastest setup; standard lead time. |
| First-time test order (any basic build) | 100 pcs | Validate design and photography. |
| Full-length 14-way divider | 200-300 pcs | Divider tube alignment raises setup. |
| Waterproof TPU / PU-coated shell | 200-300 pcs | Lamination and heat-seal steps. |
| Multi-colorway spread of one model | Per colorway | Each color is its own dye lot. |
| Order above 600 pcs | Better unit price | Full-roll material buying unlocks cost step. |
Sampling and Lead Time — Your First Timing Map
MOQ matters less than sequence if you miss your retail season. A typical custom program at our affiliated plant runs on two clocks. The first is sampling: concept and pre-production samples take 10-20 days depending on how many rounds you need and whether the logo or structure changes between rounds. The second is bulk: once the sample is sealed, production runs 45-60 days.
Plan at least one buffer round of sampling on a first program. If your retail launch is twelve weeks out, we recommend you start the sampling conversation at week one so there is room for a colorway correction or a hardware swap before the bulk clock starts. Buyers who treat sampling as a formality are the ones who compress the lead time and end up paying for air freight or a partial order.
One of the strongest planning habits we see is aligning the MOQ to a sell-through forecast rather than a gut feeling. If your historical sell-through for a carry bag is 40 units a month across your retail doors, a 200-piece first order is roughly five months of cover — which is about right for a season launch and comfortably above the minimum. Anchoring the order to a real forecast, not to the minimum, is what keeps you from both overstocking and stocking out mid-season.
Colorways, SKUs, and Inventory Discipline
The fastest way to trip over a MOQ is to spread one model across too many colorways. Every colorway is a separate dye lot and therefore a separate minimum consideration. A model in six colors is six potential minimums, and at retail the slow colors will absorb your working capital while the fast colors stock out. The disciplined approach is two to three colorways for a first season, then expand the palette only after you have sell-through evidence.
SKU discipline also touches accessories. A stand bag program often includes a rain hood, a dual strap set, and a cooler pocket. Confirm which accessories ship as standard and which are optional add-ons, because each optional variant can split your order into sub-minimums. Locking a single "base bag + hood" standard for the first season keeps the order clean and the QC line simple.
Think about the retail retail photo set as well. Most buyers photograph two to three colorways for the listing and treat the rest as replenishment. If you keep your first season tight, you spend your photography budget on shots that actually drive conversion, and you build a cleaner baseline for the reorder conversation. Every colorway you remove from the first run is capital you can spend on sell-through data for the second.
What Actually Correlates with Good Quality at Volume
Many B2B teams choose a factory on price per unit, then discover the real cost driver is quality. At our affiliated plant, quality at volume rests on three pillars: sealed samples, inline inspection, and AQL-based final checks. The sealed sample is the frozen reference unit — every batch is measured against it, not against a memory of what it should look like. Inline checks happen at cutting, sewing, assembly, and final inspection, so defects are caught while the line can still rework them cheaply.
The numbers matter here. With seven lines, 149 machines (126 sewing machines), and 137 staff, our plant runs roughly 150,000 bags a month against a validated capacity of 200,000. Running below capacity is deliberate; it gives the QC line time to hold tolerances on the stand deployment, zipper pull, and strap anchors that a fully loaded line tends to skip. When you see a factory that claims maximum output every month, ask how much inline AQL inspection it actually performs.
For buyers, the practical ask is simple: request the AQL plan, the defect-class definitions (critical, major, minor), and the acceptance/rejection numbers for the first lot before you sign. A factory that can write those numbers down is a factory that can repeat them. A factory that just says "we do quality control" without a plan is where your first-season warranty costs come from.
Negotiating the Minimum without Starting an Argument
The MOQ conversation is not a confrontation if you bring data. Start by asking for a breakdown of what the minimum covers: cutting marker, hardware buying quantity, dye lot, and sampling amortization. Factories will usually flex the minimum when the buyer commits to a forecast timelble, consolidates colorways, or takes a long-term multi-season view. A sensible middle ground is a 100-piece test order now plus a committed schedule for the full MOQ as a replenishable line.
You can also negotiate on the basis of the reorder. If you commit to a repeat season with the same sealed master and artwork, the second run has almost no setup reboot — the pattern, thread, and placement are already frozen. That repeatability is worth real money to a factory, and we typically reflect it in more flexible minimums on reorders. The best negotiating posture is "I want a repeatable program, not a one-off," because that is what lets the factory lower its own production cost and pass part of it back.
Finally, separate the MOQ from the unit price in your head. A lower minimum with a much higher unit price can cost you more over a season than a higher minimum with a better per-unit number once you add freight, warehousing, and markdown risk on overstock. Run the total landed cost on both scenarios before you negotiate; the factory will respect a buyer who is engineering for the total, not for the headline rate.
Common MOQ Mistakes First-Time Buyers Make
The most expensive MOQ mistake is designing around the size of the carton instead of the size of the sell-through. A buyer who fills a container because the freight rate looks good ends up holding inventory that eats margin in warehousing and markdowns, while a buyer who orders the minimum in too many colorways loses the volume cost break that makes the program profitable. Both errors flow from the same root cause: treating MOQ as a target to hit rather than a constraint to plan within.
A second common mistake is conflating the MOQ with the sampling quantity. Sampling is not part of the bulk minimum in our workflow — a concept sample and a pre-production sample are quoted separately, and they should be. If a factory folds sampling into the MOQ, press for the breakdown, because it usually hides setup cost that will reappear in the unit price later. Keep the sample approvals, the sealed master, and the bulk run as three clearly separated budget lines.
The last and most damaging mistake is skipping the pilot-run inspection log. Many buyers approve a sample, then never look at the first-article report on run unit #1. When the line drifts between the sample and the first hundred units, that drift becomes the baseline for the whole season. Ask for the first-article inspection and the defect photos before the run continues past the first carton; catching a drift at unit twenty is nearly free, while catching it at unit two thousand is a rework or a claim.
Reading a Factory's MOQ Term Sheet Like a Pro
When a factory sends you a MOQ term sheet, read it line by line rather than skimming to the minimum number. Three clauses decide whether the deal works. First, whether the MOQ is per model, per colorway, or per article number — a "200-piece MOQ" that applies per colorway is a very different commitment than one that applies to the total order. Second, whether the minimum includes sample pieces or is bulk-only after sampling is quoted separately. Third, whether the lead time clock starts at sample approval or at order confirmation, which shifts your season planning by weeks.
You should also check how the factory treats reorders. A genuine repeatable program should carry a lower effective minimum on replenishment because the setup is already frozen. If the term sheet quotes the same high minimum on every reorder regardless of the sealed master, it is pricing the relationship as a string of one-offs. At QUANZHOU JUNYUAN BAGS we price reorders on the frozen records we keep for the life of the program, which is why our replenishment minimums are typically more flexible than the first-run number.
Finally, confirm how freight and Incoterms interact with the minimum. A FOB price assumes the buyer handles the ocean leg, while a DDP price bundles freight, duty, and delivery into one figure. The same 200-piece order can look very different on a DDP quote because the inland delivery and clearance costs are amortized across a small carton. Decide your Incoterms before comparing totals, and if you are still undecided, our Incoterms guide lays out the practical trade-offs for stand bag freight.
First-Order Checklist Before You Send the PO
A clean first order is the difference between a smooth season and a painful one. Confirm the model and divider spec, lock the material and denier, list every pocket and its access logic, define the logo method and placement with coordinates, and write down the colorway and quantity per SKU. Then agree the AQL plan, the functional tests for the stand and zippers, and the sampling timeline.
Document every decision in a one-page tech pack. The buyers who move fastest send the tech pack with the first RFQ, because it lets us quote the true cost instead of a generic number. Include your target market, expected MOQ, and reference photos, and we will return a sampling plan inside 24 hours. If you are early in the process, our golf stand bag buying guide walks through the same variables.
Do not finalize the PO until you have approved a sealed pre-production sample on the actual production fabric. The sample is your legal and physical contract for the run; if it is not right on the sample, it will not be right in bulk. Our factory and QC page shows the inline checkpoints our affiliated plant runs at each stage.
Beyond the MOQ — Building a Reorderable Program
The real goal of understanding the MOQ is to build a program you can reorder without rediscovering the setup. When the first run is complete, three records make a reorder cheap: the sealed master unit, the approved color chips, and the AQL inspection log for the last lot. With those, a second or third season is a straight repeat rather than a new project, and the effective minimum on replenishment is often lower because nothing has to be reconfigured.
This is where working with an affiliated factory with its own QC depth pays off. Because our plant holds 20 years of industry experience, 200+ brands served, and exports to 100+ countries, we have the pattern library and the hardware stock to turn a reorder around faster. The MOQ you negotiate on year one becomes a relationship, not a wall, on year two.
If you are comparing us to other stand bag suppliers, bring the same three records to every quote: your tech pack, your target quantities per colorway, and your inspection standard. We will quote honestly against the MOQ, the lead time, and the QC plan, and we will flag anywhere the numbers do not pencil. That is the difference between a factory pricing a carton and a partner pricing a program.
Test Plan & Acceptance Criteria
For professional programs, add test methods and pass/fail criteria so the MOQ conversation is backed by measurable targets rather than opinion. The most important checks for a stand bag are the stand deployment cycle, zipper durability, and strap anchor load, because those are the mechanical parts that fail first on the course.
- Stand deployment cycle test — 3,000-10,000 cycles with no cracking or severe wobble.
- Zipper smoothness and jam-rate test with a defined pull force.
- Strap anchor static load test with a defined stitch-failure criteria.
- Fabric abrasion test on the lower panel and wear plate.
- Packed drop test to the carton spec with corner/edge/face drops.
- First-article inspection on run unit #1, recorded with defect photos.
Recommended Internal Links
- Products (Stand Bag Architectures)
- OEM/ODM Service
- Factory & QC
- Golf Stand Bag Buying Guide
- What Drives Stand Bag Cost & Pricing
- Lead Time Planning: Sample to Mass Production
FAQ
What is the typical MOQ for a custom golf stand bag?
At our Quanzhou operation the regular MOQ is 200 pieces per model per colorway, and we accept a 100-piece trial order for first-time brand validation. Sample development runs 10-20 days and bulk production 45-60 days.
Why do factories set a minimum order quantity for stand bags?
The MOQ exists because cutting, sewing, hardware setup, and colorway dye lots have fixed setup costs. Below roughly 100-200 units the per-bag setup is uneconomical and the factory cannot hold a stable color or stitch standard.
Can I order fewer units to test my golf stand bag line?
Yes. We support a 100-piece test order so you can validate the product, photography, and retail feedback before committing to a full run at the regular 200-piece MOQ.
Does the MOQ change with 14-way dividers or waterproof fabric?
Complicated architectures such as 14-way dividers or TPU waterproof panels may carry a slightly higher MOQ because of mold and lamination setup. Basic 4/5/6-way nylon and polyester builds stay at the standard MOQ.
What matters more than MOQ when choosing a stand bag factory?
Repeatability and QC. Our SGS-verified affiliated plant (4,950 sqm, 7 lines, 149 machines, 137 staff, ~150,000 bags a month) runs AQL-based inspection and keeps a sealed master so your second season matches your first.
How do lead time and MOQ interact on my first order?
Sampling takes 10-20 days and bulk production 45-60 days. If you plan sampling and pilot together with your retail launch date, a smaller first MOQ lets you de-risk while still hitting the season window.
What should I send with my quote request to lock the right MOQ?
Send bag type, divider (4/5/6/14-way), material direction, pocket list, logo method, expected quantity per colorway, and your target market so we can recommend the minimum viable order.
Request a B2B quote for golf stand bags
Send your target market, expected MOQ, and reference photos. We respond within 24 hours with a sampling plan.