Material is the biggest single driver of a custom golf stand bag's weight, cost, and durability — switching a shell from standard polyester to a heavier nylon or adding a TPU waterproof package can move unit cost by 10-20%, so naming the fabric and reinforcement before sampling is what controls your landed price. This guide walks a B2B buyer through the main stand bag materials — polyester, nylon, PU synthetic leather, and waterproof TPU laminates — how each performs on weight, feel, and abrasion, and the test targets and QC checkpoints that keep a material choice repeatable across a full run. It draws on the material practice of an SGS-verified Quanzhou facility (4,950 sqm, 7 lines, 149 machines, 137 staff). For brands that want a fully customized silhouette — structure, dividers, pockets and hardware — our custom golf bag factory team specializes in OEM/ODM programs.
Key Takeaways
Hold these five rules before you brief. First, state the shell, lining, denier, and finish by name, not by a color or a vague style label. Second, match the material to the weight target and price band — a value walker runs thin polyester, a premium line adds PU panels. Third, decide the waterproof scope explicitly; a coated fabric is not the same as a sealed waterproof package. Fourth, define the reinforcement scope at stress points, because that is where cheap bags tear. Fifth, lock test targets — abrasion, tear, seam strength, colorfastness — into the brief so samples and bulk read the same bar.
- Name shell, lining, denier, and finish on the physical brief
- Match material to weight target and price position
- Define the waterproof scope separately from material type
- Lock reinforcement scope at the stress points
- Set abrasion, tear, seam, and colorfastness test targets
The Material Cost and Weight Lever
Material is not a decoration; it is the largest line of your bill of materials. Moving from a standard polyester shell to a heavier 600D nylon raises both weight and per-meter cost, and adding a TPU laminate or a PU panel layer drives cost further. Buyers who understand this negotiate with the material, not against the factory: you trade weight and feel for cost in visible, inspectable steps. Knowing which material direction each segment requires lets you price honestly and protects margin on every SKU.
The lever works both ways. A premium bag that sells on PU trim and refined hardware must budget for those materials; a value bag that must hit a retail floor has to hold material cost low. Write the intended retail price and target weight beside the material choice, and let the three stay consistent. When the material, price, and weight line up, the sample proves the story, and bulk production holds it, keeping every unit in the run true to the promised spec.
Polyester: The Light, Clean-Value Standard
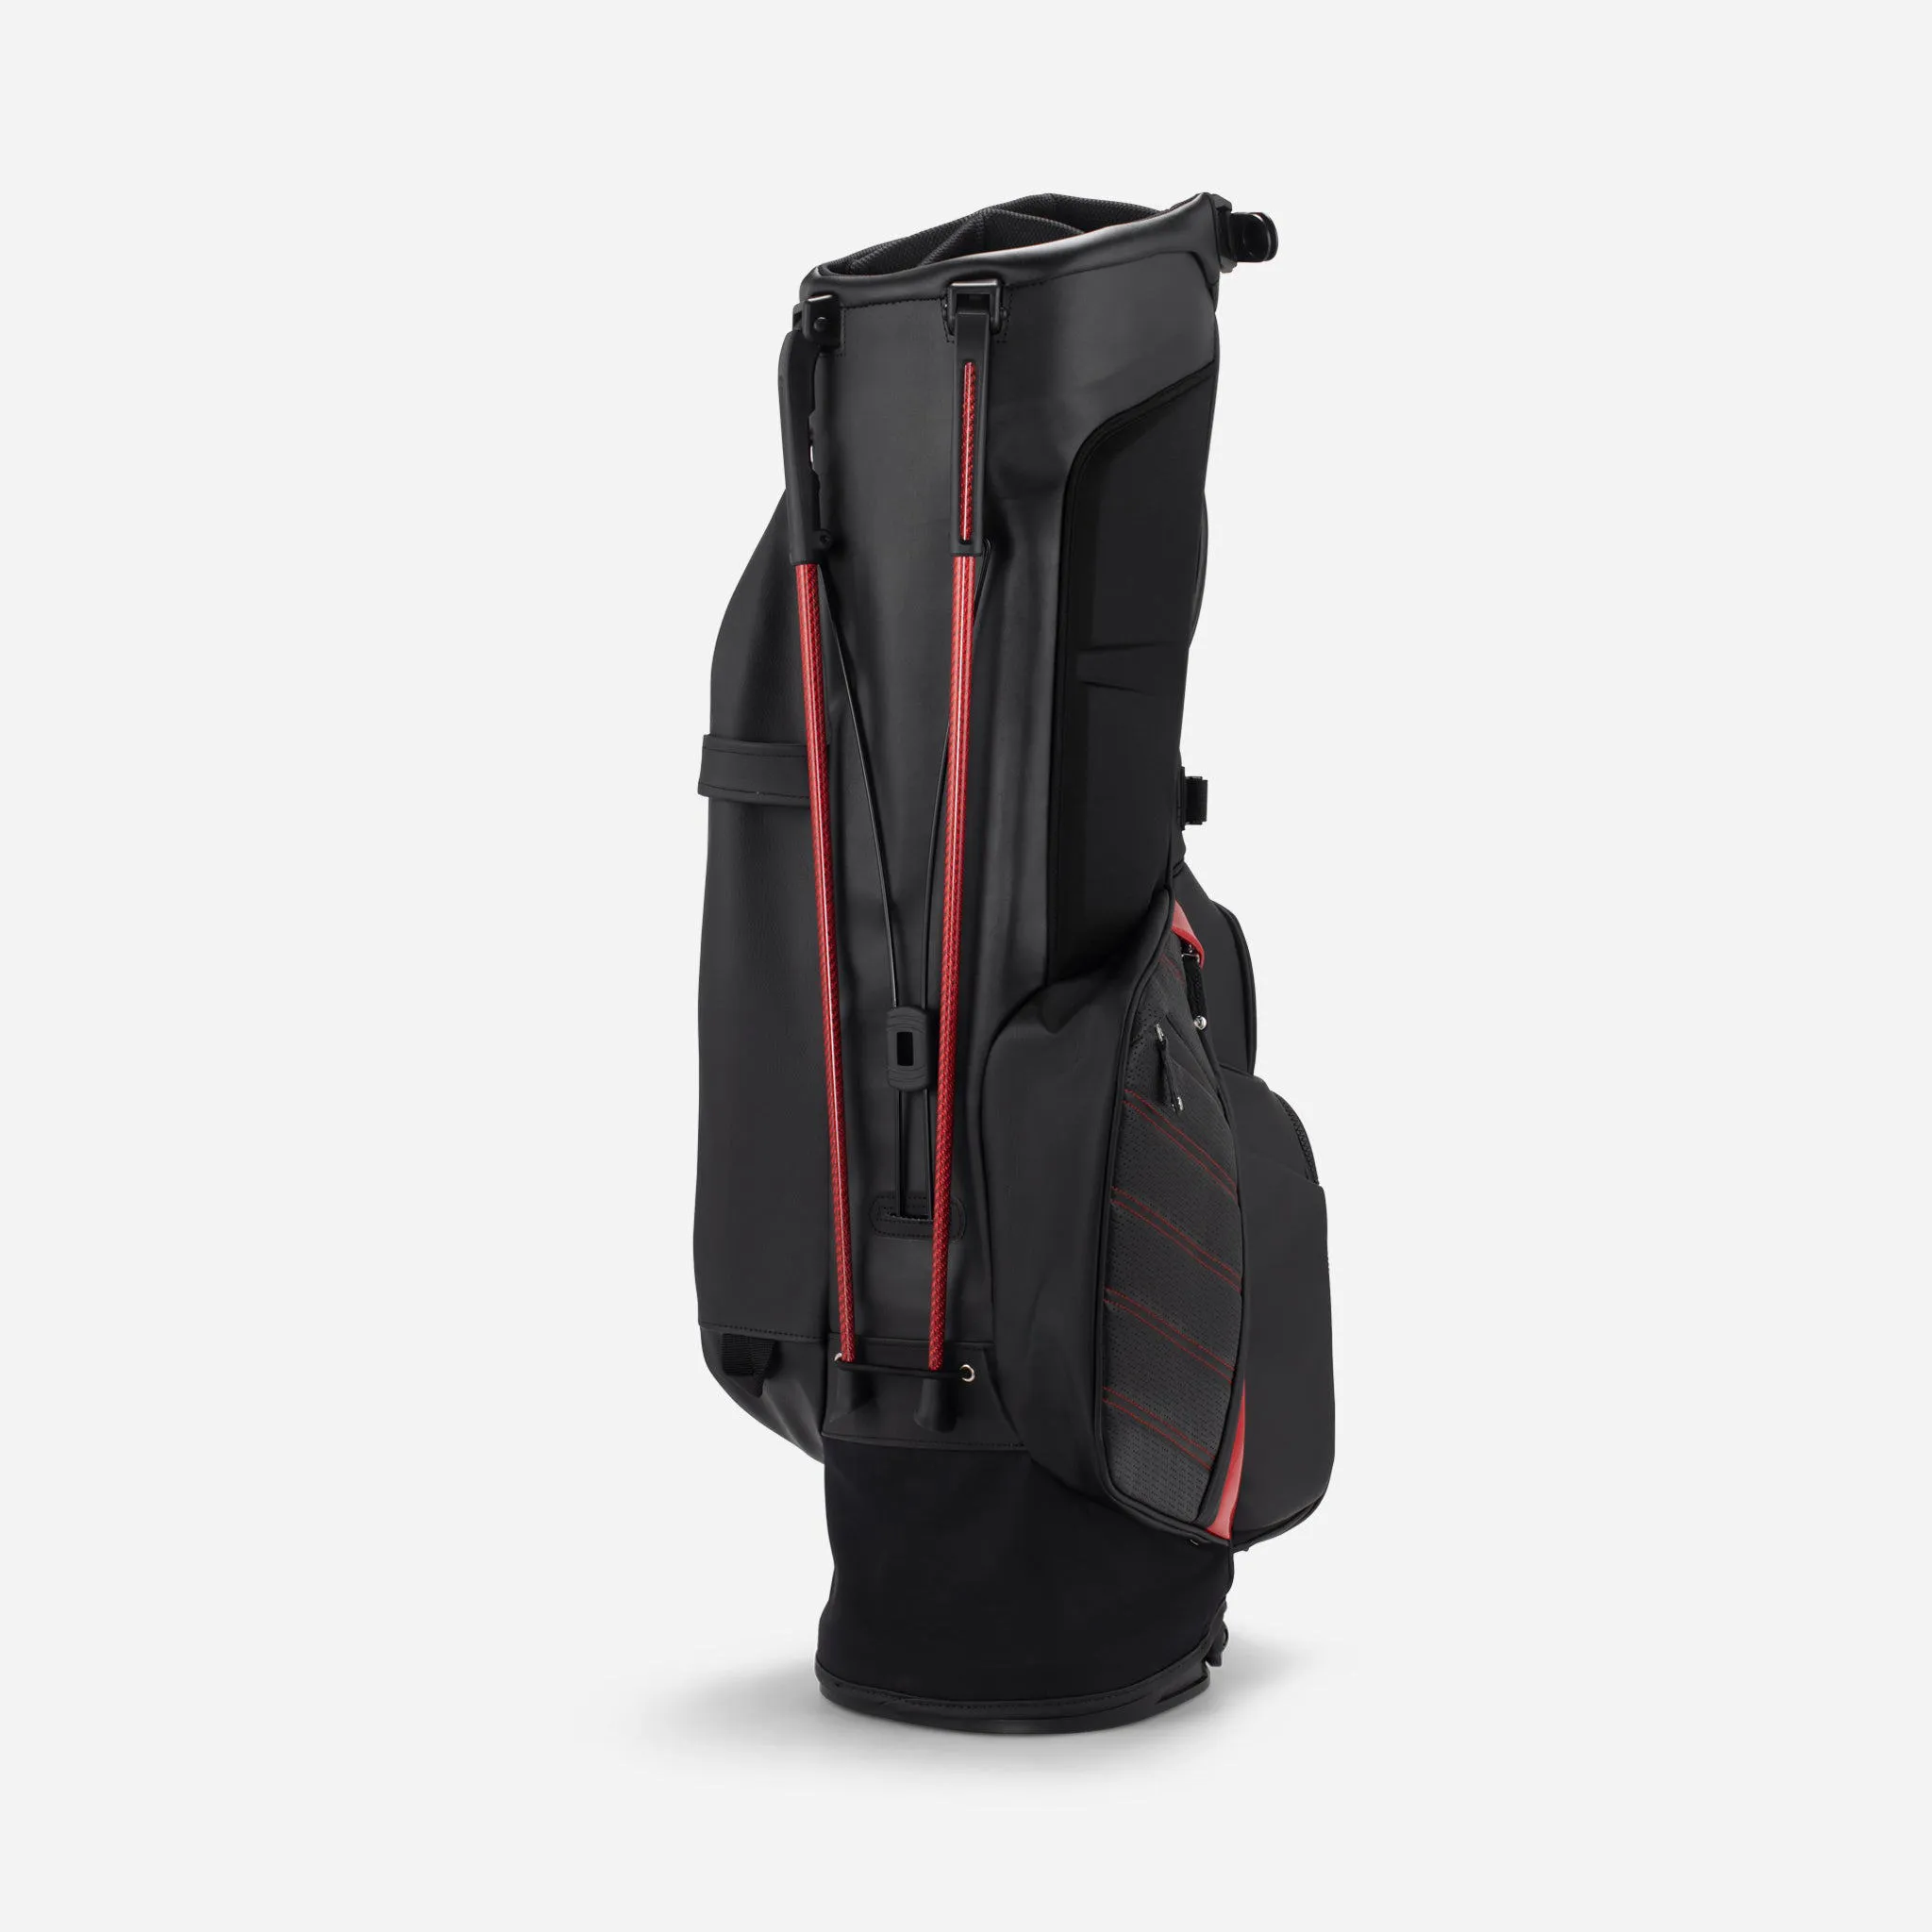
Polyester is a dependable default for value and mid-tier stand bags. It is relatively light, dries well, and prints and dyes cleanly with a smooth hand, which makes it popular for panels that carry bold graphics or strong colors. At common grades of 300D to 600D it balances weight, cost, and a presentable finish, and it holds bright brand color well. For a catalog chasing entry-level volume with a clean look, polyester is often the right first shell.
Its trade-off is abrasion resistance on heavy course use: polyester is generally less rugged than a comparable nylon at the same denier, so it is best kept off the highest-wear zones on a full round bag. Reinforcement at the base, stand attachment, and strap anchors compensates for this. If a buyer runs a mixed catalog, a common approach is a polyester shell with nylon reinforcement panels at the stress points — the look of polyester where it matters, the toughness of nylon where the load lands.
Nylon: The Abrasion-Resistant Durable Choice
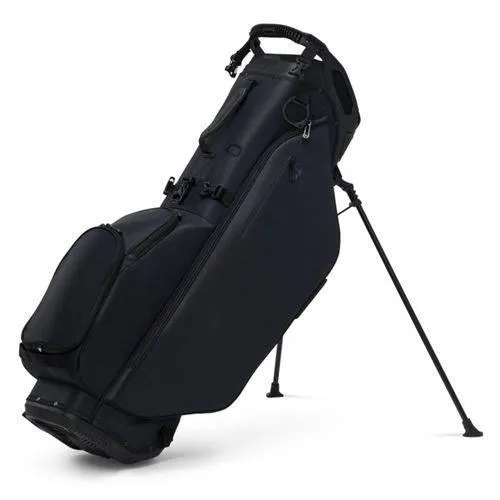
Nylon, especially in 400D to 600D and up, is the go-to material for stand bags that must survive repeated course use. It resists abrasion well, holds color, and takes a tight weave that feels more substantial than polyester of the same weight. For a walking bag that gets set down, dragged, and bumped shot after shot, nylon's toughness at stress zones is exactly what protects the bag from premature wear and returns. It is the material most commonly chosen for mid-tier and premium carry lines.
Nylon does have nuance: higher denier means more weight, and some nylon finishes are more prone to a slight sheen or require a coating to control it. In our line we specify not just the denier but the finish and any coating, because the same "nylon" can vary by hand. Confirm the actual swatch on the sample rather than relying on a name alone. When nylon is matched to the right weight target and reinforced at the seams, it is the most durable honest choice for a bag customers will actually carry.
PU Synthetic Leather: The Premium Feel Layer
PU synthetic leather raises perceived value on a stand bag without the cost and maintenance of real leather. Used on panels, the lid, or a branding patch, PU gives a refined, furniture-grade look that reads premium in retail photography and in the hand. It is a common choice for premium and tour-positioned lines where the buyer wants a bag that looks expensive on the shelf, and it layers well into a mixed shell where leather-look panels sit beside nylon for the carry zones.
The discipline with PU is weight and durability. PU panels weigh more than plain fabric and, depending on the substrate and coating, can be less abrasion-resistant on high-wear seats, so they belong on decorative or lightly-loaded panels rather than on the base and strap anchors. Confirm the PU grain and coating on the actual swatch, because the range of quality is wide. Used where the look matters and reinforced where the load lands, PU gives a premium finish that still survives a full season of play.
| Material | Best For | Typical Denier / Form | Weight & Cost Notes |
|---|---|---|---|
| Polyester | Value / mid-tier shells, bold graphics | 300D-600D | Lighter, cheaper, good color; reinforce stress zones. |
| Nylon | Mid-tier / premium carry shells | 400D-600D and up | Abrasion-resistant, substantial; higher denier adds weight. |
| PU synthetic leather | Premium panels, lid, branding patch | Coated/substrate layers | Premium look; heavier, place off high-wear zones. |
| TPU-coated / laminated | Waterproof programs | Coated or laminated shell | Protects contents; adds weight and seams to manage. |
Waterproof Materials and the Scope Spectrum
Waterproofing is a construction decision, not just a material label. At one end, a standard fabric may be splash-resistant. In the middle, a coated fabric sheds light rain for a few holes. At the other end, a sealed waterproof package — a TPU-coated or laminated shell with taped seams and water-resistant zippers — protects the contents in a genuine downpour. Because these levels cost very differently, define which one your buyer needs before you lock the material.
A common error is assuming a waterproof-looking material makes the whole bag waterproof. A decorative PU panel or a coated outer layer does not protect the valuables pocket if the seams leak. In our waterproof programs we confirm the seam-taping scope, the zipper standard, and which openings are sealed, then test the result rather than trust the label. Matching the waterproof scope to the use case prevents paying for a package nobody needs and missing the protection that rainy-market buyers do need.
Reinforcement: Where Cheap Bags Come Undone
Reinforcement is the difference between a bag that lasts and one that tears on the tenth round. The stand attachment panel, the two strap anchors, the base wear plate, and the pocket mouths carry the highest load and need heavier stitching and backing than the general shell. A budget cut in production will often remove exactly this reinforcement, so put it in the brief by name and make it non-negotiable. Confirming the reinforcement scope up front is what protects your warranty and your reputation.
Reinforcement is also where the material meets the thread. A thin shell with dense stress-point stitching needs a backing film or a bar-tack pattern that spreads the load, and the seam strength at those seams should be tested, not assumed. In our QC we specify seam strength at stress points and inspect them inline. When the material, thread, and reinforcement are locked together, a stand bag survives the abuse that defines the category.
Hardware, Stitching, and Trim Grades
The material also sets what hardware and stitching can be used on it. A thin nylon panel flexes differently under embroidery than a heavier PU panel, so the logo method has to match the fabric to avoid puckering or peeling. Similarly, zippers, pulls, and buckles chosen for one shell may not suit a heavier waterproof one. Brief the hardware grade and stitching density alongside the material, so the whole construction is consistent rather than bolted together from mismatched parts.
Consistency is the trap in bulk. If the zipper standard or thread grade drifts between batches, the same material can produce two different products. In our line we color-band trims against the shell, lock the zipper standard, and confirm the finish on the sample. Getting the hardware and stitching to sit under the material rather than fight it is what makes a spec read as one product across a full run.
Test Targets You Should Lock Into the Brief
A material choice needs measurable acceptance targets, not just a photogenic swatch. Define the tests and their pass/fail lines in the brief: fabric abrasion (about 20,000-50,000 cycles by a defined method), tear strength at the reinforcement seams, seam strength at the stress points, and colorfastness or fade against a sealed chip with a set delta-E. Also state the sampling method and accepted quality level so both sides inspect to the same defect bar.
These numbers turn a material from a taste judgment into an auditable spec. When a batch arrives, the QC line checks the fabric against the locked targets rather than against a memory of the sample. That audit trail is what protects a reorder: the second season's material must meet the same abrasion and tear numbers as the first. Lock the targets, and the material is repeatable; leave them vague, and every run is a new gamble.
Colorways and Dye-Lot Consistency
The best material spec fails if the color drifts across batches. For every colorway, approve a lab-dip or a physical color chip, assign a Pantone reference rather than a screen approximation, and set a dye-lot tolerance so a fabric or thread lot change never shifts the tone. This discipline is non-negotiable for a branded line, because a tonal mismatch across thousands of units is one of the fastest ways to look careless at retail.
Keep a sealed master unit from the approved sample for the life of the program. On reorders, the QC line compares every inspected unit against that master, so a relaunch two seasons later matches the original colorway. This is the concrete mechanism behind a repeatable brand, and it is cheap insurance compared with the cost and reputation damage of a color mismatch in production.
Match the Material to Your Sampling Plan
Because material behaves differently across the shell, the pre-production sample must be made on the exact production fabric with the final reinforcement and hardware. A sample made on a different swatch does not prove the bulk will feel or wear the same. Budget for the right number of sample rounds — one to validate look, and one to lock the technical file on a first-time material or complex construction — and confirm who owns revision costs before you start.
With sampling at 10-20 days and bulk production at 45-60 days, a realistic plan spaces a test order before the full run so field feedback on the material lands before you commit. Our test-order MOQ supports this at around 100 units, with a regular order at 200 units per colorway. Field data on how the material feels after a real round is worth more than another design meeting, and it catches the small issues no photograph shows.
Lining, Backing, and Internal Construction
The visible shell is only half the material story; the lining and backing decide how the bag feels inside and how it holds its shape. A smooth, hard-wearing lining protects clubs and pockets and makes the bag feel more finished, while a soft lining adds a premium in-hand feel but can show wear under heavy club weight. The backing film behind stress-point stitching spreads load and prevents tearing. Name the lining and confirm the backing scope in the brief, because these are easy to cut in production and impossible to see in a surface photo.
Internal construction also affects weight more than most buyers expect. A fully padded or a heavily backed bag quietly gains weight that pushes it out of its target band. In our line we match the lining and backing to the weight target, using reinforcement where the load actually lands rather than padding the whole shell. Confirming the internal construction on the pre-production sample, not just the outer material, is what keeps the promised weight, feel, and durability in the unit your customer opens.
Material Selection by Segment and Price Point
Material is also the fastest way to cut or inflate cost per segment. A value entry bag holds its price by using lighter polyester and less backing; a mid-tier bag lifts perceived quality with nylon and upgraded zippers; a premium bag earns its price through PU panels, refined trims, and tighter stitching; an all-weather bag spends on the waterproof package. Pairing each segment with the right material keeps every SKU competitive at its shelf price while protecting margin.
The mistake is chasing premium material on a value SKU or thinning a premium one to save a few cents. Both readers as a mismatch at retail. The discipline is to write the price band, weight target, and material direction on one line for every SKU, and to let the sample confirm the three stay consistent. When material, price, and weight are locked together per segment, a catalog is easier to source, cheaper to hold, and more honest on the shelf.
Common Material Failures and Their Prevention
Know the failure modes each material introduces so your QC plan is built around them. A thin polyester shell can tear at the strap anchors if the reinforcement scope is adrift. A nylon clearcoat can rub and fade on the seat if the wrong finish is chosen. A PU panel can crack or peel at the flex line of the stand hinge if placed where the bag bends. A waterproof package can leak at a seam that was not taped. Name the top three failures you fear for your material choice and put a test in front of each one.
We build QC checkpoints around exactly these risks: seam strength at the anchors, abrasion and colorfastness on the seat and logo panel, tape integrity on a waterproof package, and a flex check near the hinge. Because the material decides which fields matter, a generic checklist is not enough. A custom program earns its name when the inspection record is built from its own material's failure modes, so a defect is caught in line instead of at the container.
Procurement Worksheet for Your RFQ
| Requirement | Your Target | Notes / Questions |
|---|---|---|
| Shell material & denier | Polyester / nylon / PU; 300D-600D or coated? | |
| Lining & finish | Lining type, coating, hand preference? | |
| Waterproof scope | Standard, coated, or sealed package? | |
| Reinforcement points | Stand panel, strap anchors, base, pocket mouths? | |
| Hardware & trims | Zipper, pulls, buckles; finish and color-band? | |
| Test targets | Abrasion, tear, seam strength, colorfastness? | |
| Colorway & chip | Pantone refs, lab-dip approval, dye-lot tolerance? | |
| MOQ & lead time | Test order, regular order, sampling plan? |
Recommended Internal Links
- Products (Stand Bag Architectures)
- OEM/ODM Service
- Factory & QC
- Golf Stand Bag Buying Guide
- Stand Bag Materials Guide
- Choosing the Right Custom Stand Bag
FAQ
Is nylon or polyester better for a golf stand bag?
Both work well. Nylon, especially 600D and above, is more abrasion-resistant and holds color well; polyester is often lighter and cheaper with a clean look. Choose by weight target, wash performance, and budget.
How does material choice affect stand bag weight?
Material is the single biggest driver of weight. Lightweight lines use 400D nylon or thin polyester; premium lines add PU panels and upgraded trims; waterproof bags add coated fabric and seam tape, all of which raise weight.
Can you use PU synthetic leather on a waterproof stand bag?
You can, but waterproofing depends on the construction: a coated or laminated TPU shell with taped seams protects contents, while decorative PU panels may not. Define the waterproof scope explicitly rather than assuming the material makes it waterproof.
What material test standards should a buyer request?
Ask for an abrasion test (such as 20,000-50,000 cycles by a defined method), tear strength at seams, seam strength at stress points, and a colorfastness or fade test against a sealed chip.
Why do reinforced stress points matter on a stand bag?
The stand attachment panel, strap anchors, and base wear plate carry the most load. Reinforcing these seams and panels prevents tearing and returns, so define the reinforcement scope rather than letting production cut it.
Do you support OEM/ODM for golf stand bags?
Yes. We support OEM (branding on proven architectures) and ODM (co-develop structure, pockets, materials, and hardware). Provide your target market and quantity to start.
Request a B2B quote for golf stand bags
Send your target market, expected MOQ, and reference photos. We respond within 24 hours with a sampling plan.